Insulation industry

Where the packmisses the spec

The melt is already running. Recycled glass or slag that is dirty enough changes the fiber. Density and R-value are confirmed after the pack. The line still has to run.

  • 01

    Heat spent on this melt, not the last one

    Read furnace or cupola tags the plant already logs, so extra fuel is not the only answer when cullet, slag or pull changes.

  • 02

    Fiber that matches this pack

    Hold diameter, shot and density against the recipe from the line and lab records you already keep — not after the warehouse finds the off-spec.

  • 03

    The oven stop while it can still be planned

    Read forming, curing-oven and fan signals already in the historian, so a bearing or a zone failure is not the first notice.

On the melt and the line

Quality is decided before the pack

Insulation plants lose money in three places that rarely share one screen: a tank or cupola that is burning more than the pull needs, recycled glass or slag that is too dirty to raise, and a density or binder miss found after the pack. Most of that is already in historian tags, batch tickets and lab records — after the fact.

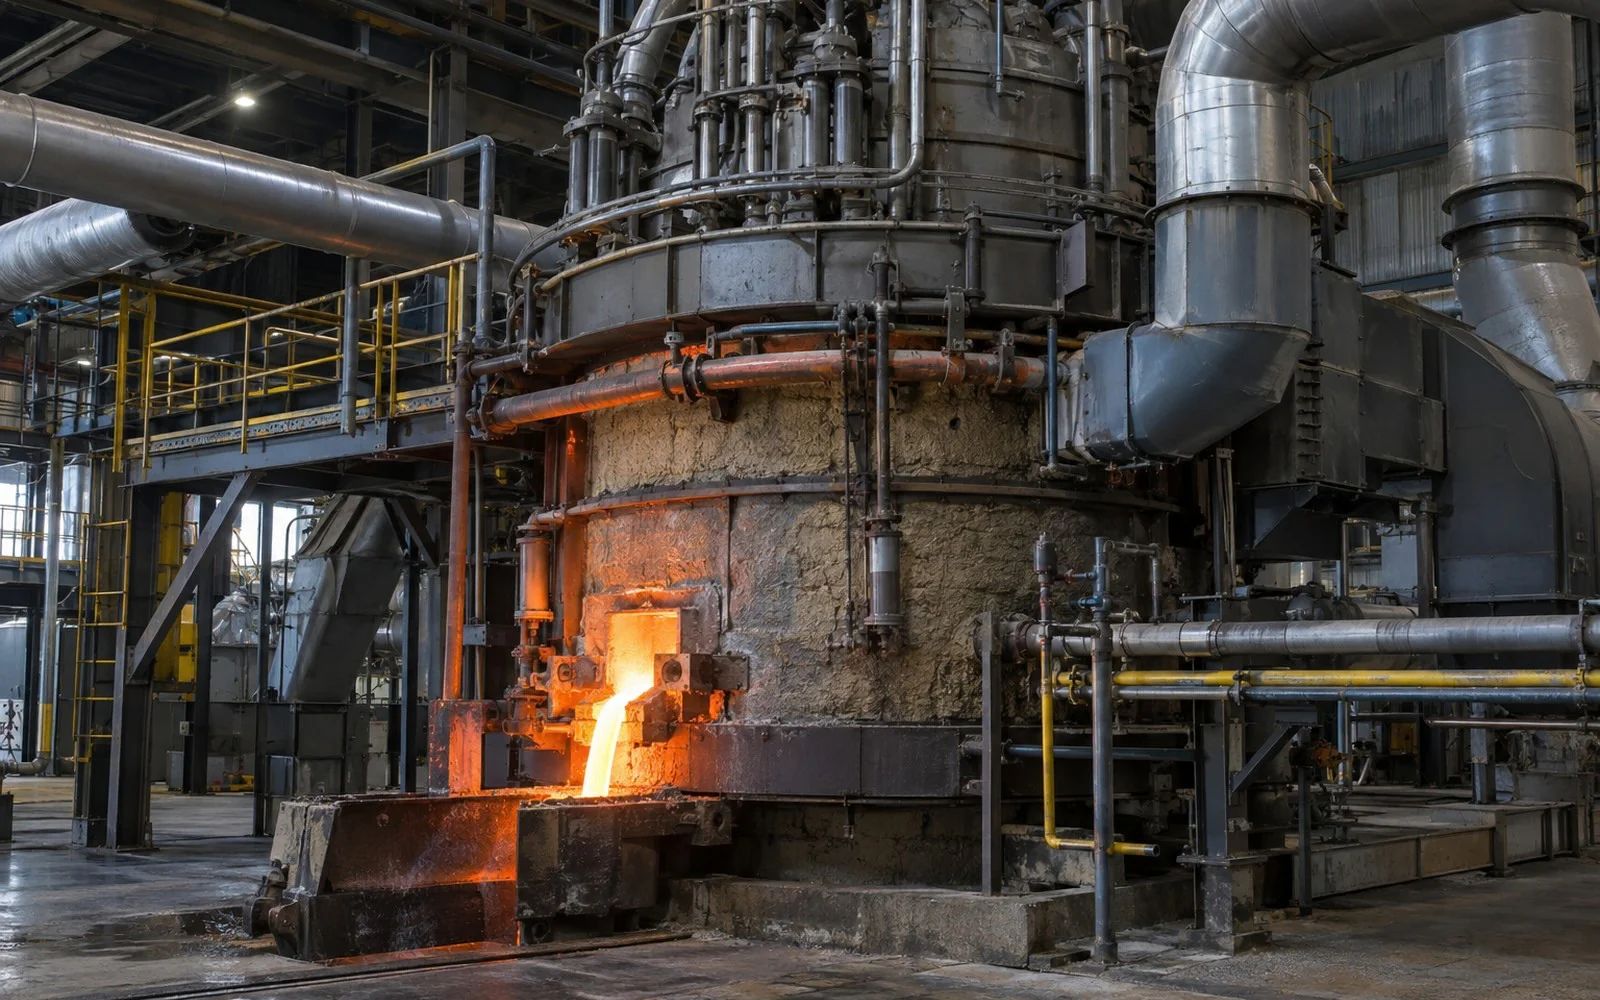
Industrial energy and combustion systems under continuous loadThe melt

The furnace does not stop. The fuel bill does not either.

Fiberglass plants melt siliceous batch in high-temperature furnaces. EPA's 2019 plant study put the median carbon intensity at 0.483 tonnes of CO₂e per tonne of fiberglass — from on-site fuel and process emissions. A conservative crown or cupola temperature is how many lines stay safe, and how many extra units of fuel are burned.
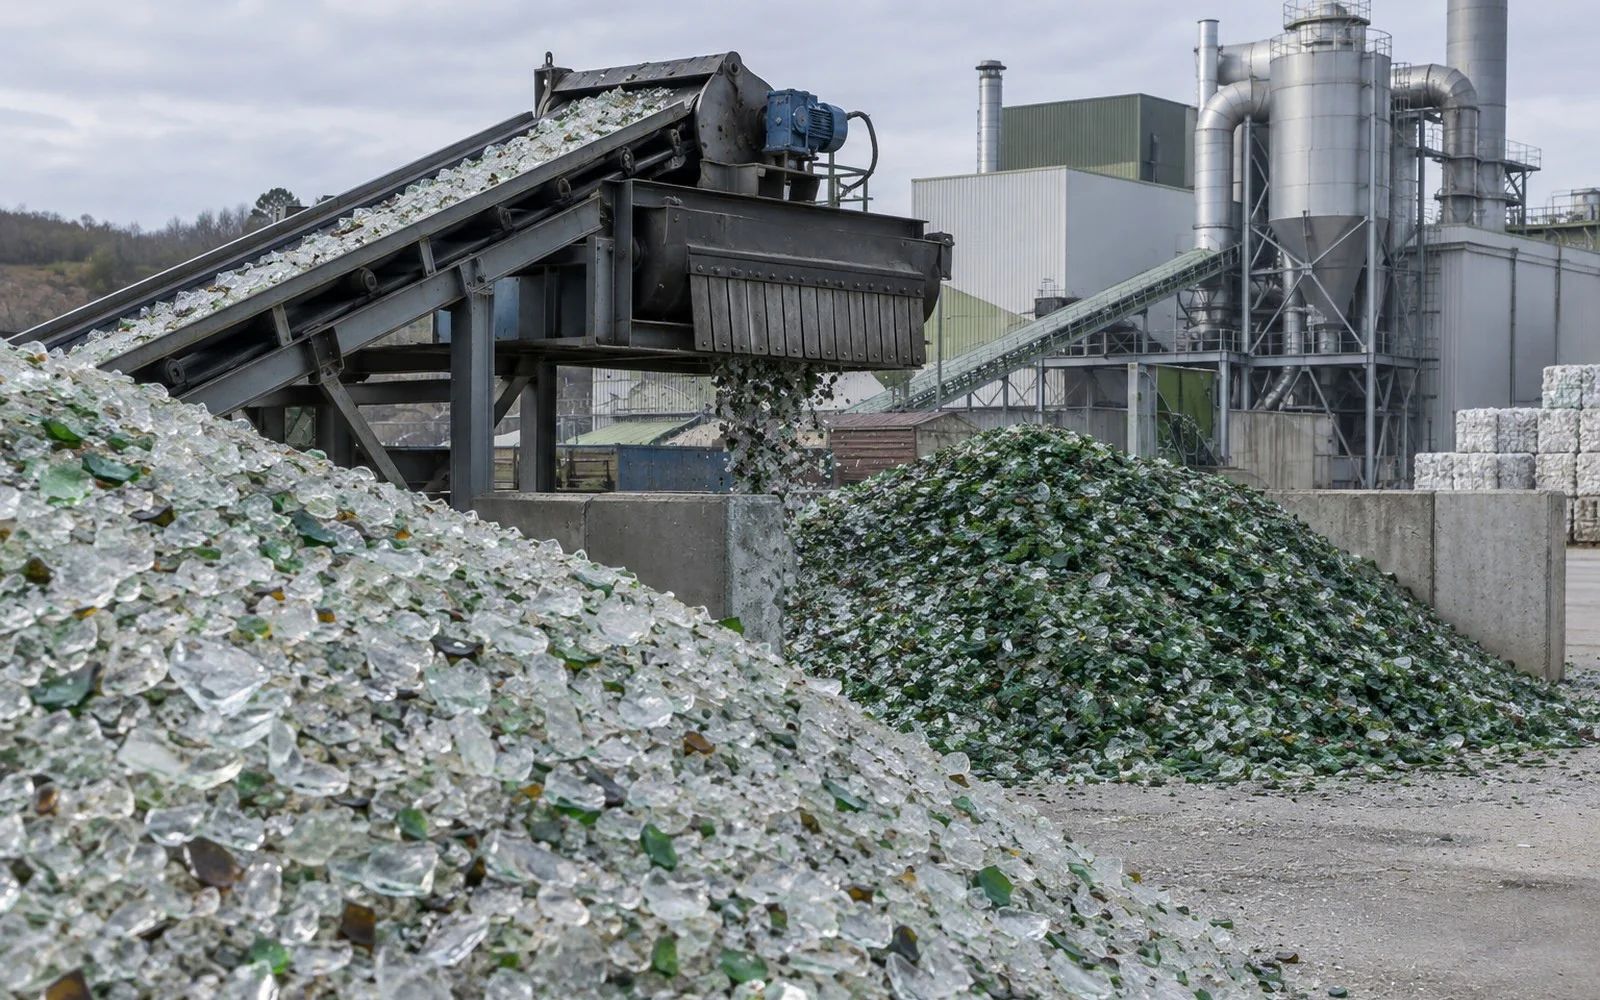
Materials plant and yard of the kind used to handle recycled glass and mineral feedThe cullet

Dirty recycled glass is still a melt problem

NAIMA members used more than 2.4 billion pounds of recycled glass in US insulation plants in 2025. Fiberglass often carries about 50% recycled glass. Metal, organics or mixed colour in that stream still show up as shot, weak fiber or a foamy tank.

Plant team reviewing process and quality readingsThe pack

Density and binder are confirmed after the wool has left

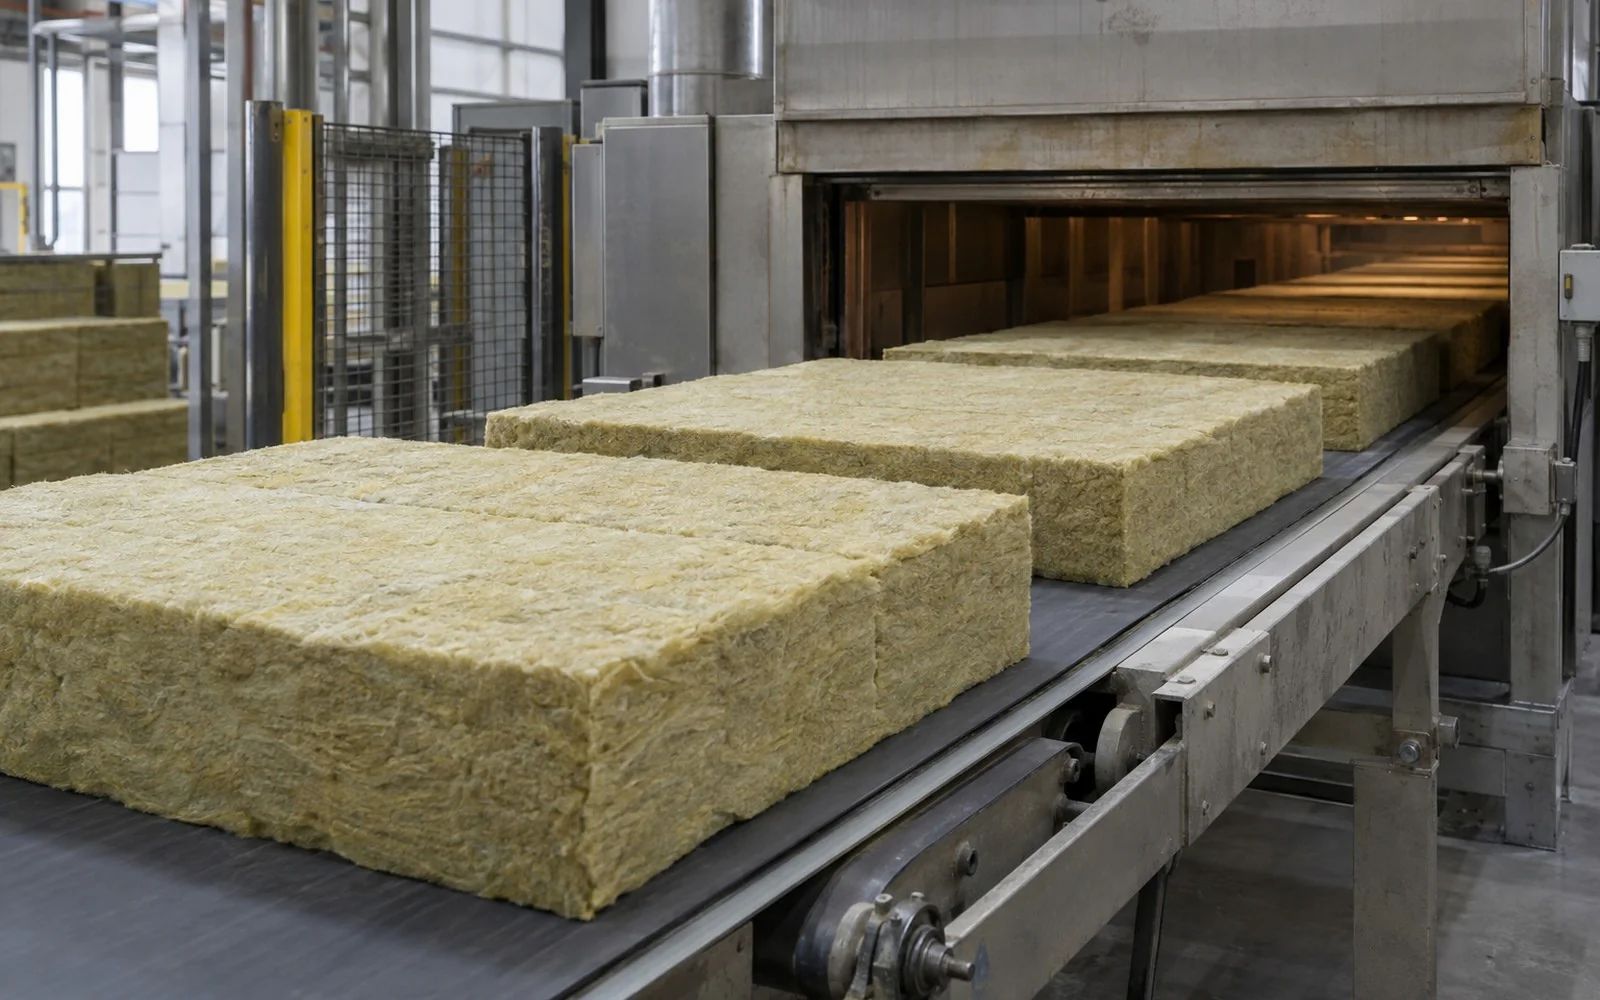
Fiber diameter, shot, density and the cure are still often checked on the cold pack or in the lab. The hours of wool that produced them are already boxed. A binder or oven drift is then a claim, not a setpoint you can still change.

Turning the furnace up is the easy correction. It is also how the campaign is spent.

INSUS works from the furnace tags, batch tickets, recycled-content records and inspection results a plant already keeps. If the gap is a dirty magnet, a drifting oven zone or a density gauge, that is what we will say.

Explore the possibilities

Industry figures

The scale of what is being decided

Four external figures, each with its source. Nothing on this page is an estimate we made up. Where we cannot cite a number, we describe the situation in words instead.

Recycled

2.9B lb

of recycled glass and slag were used by NAIMA member plants in the United States and Canada in 2025 to make thermal and acoustical insulation.

Source: NAIMA, recycled content use in 2025

Cullet

~50%

is the average recycled-glass content NAIMA cites for today's fiberglass insulation, up to about 60% depending on the plant. The cut in virgin batch only lands if that glass is clean enough to melt.

Source: NAIMA, Materials for a Sustainable Planet (N012)

High-temperature industrial process plant of the kind used for continuous melting operations

Common problems

Problems that cost you before you notice

None of these show up as a single alarm. They show up in extra fuel, a declared-value margin carried in density, and retrofit jobs that only get inspected after a complaint.

  1. The melt burns more fuel than the pull needs

    Fiberglass and mineral-wool lines melt batch in a furnace or a cupola that is built to run. When cullet, slag or moisture changes, the safe move is still more heat. EPA's plant study shows how wide the carbon intensity can run from one site to the next.

    See: Mineral Wool Melting & Curing Energy Optimization
  2. Fiber and density are confirmed after the pack

    Diameter, shot and density decide R-value and handling. They are still often checked on a sample of production. The other packs have already left the line — and declared lambda still has to carry the variation that production already created.

    See: Insulation Declared Lambda Optimization
  3. Retrofit programmes generate more jobs than inspectors can cover

    Evidence packs can look complete while the installation still carries remediation risk. At programme scale, random sampling leaves limited inspection capacity chasing the wrong jobs.

    See: Retrofit Installation Compliance Triage

Use cases

Places worth a closer look

Each is a specific starting point — this furnace and oven, this declared value, this retrofit programme — and a next conversation if it is worth your time.

Mineral wool production line showing melting furnace, fiberising and curing oven with energy optimization
Energy

Mineral Wool Melting & Curing Energy Optimization

Recommend furnace and curing-oven settings from plant historian, energy and quality data so teams can cut energy and CO2 per tonne inside a stable melt and cure envelope.

See the full use case
Distribution of mineral wool thermal conductivity results showing the difference between mean lambda and declared lambda
Quality

Insulation Declared Lambda Optimization

Model thermal-conductivity variation on mineral wool lines from process and heat-flow-meter history so teams can review declared lambda margin and density trade-offs.

See the full use case
Funnel showing retrofit insulation jobs narrowed to a risk-ranked inspection subset
Quality assurance

Retrofit Installation Compliance Triage

Rank retrofit insulation jobs by inspection risk from existing evidence packs and historical outcomes so limited audit capacity focuses on jobs most likely to need remediation.

See the full use case

FAQ

Questions that come up in every first call

A practical look at what INSUS needs, where it fits and what your team can expect.

The work that fits starts from data you already hold: furnace and curing-oven tags for energy intensity, process and lab records for declared lambda variation, and retrofit job documentation for inspection triage. Closed-loop furnace control and automatic certification of every installation are not promises we will make.

Usually not for melt records, density checks and maintenance. Most lines already have furnace or cupola instruments, a batch house, some cullet or slag handling and a curing oven. If a gauge has been drifting or a magnet is unread, that comes before any model.

No. The person who knows this tank, this recycled pile and this density spec stays responsible. The aim is to stop the next shift running extra heat from habit, and to flag a dirty load before it is a high-shot pack.

No. R-value depends on fiber, density, binder and how the product is installed. Recycled content depends on what the yard can actually supply clean. We will not invent a detection rate or a substitution target.

No. It advises the operator or the process engineer. Existing combustion systems, PLCs and any APC stay in charge of the loop. Safety interlocks and HAP controls are not touched.

It is the average NAIMA cites for fiberglass insulation, not a measurement of your line. Mineral wool uses slag at different rates. Your charged tickets are the number that matters.

Yes. The approach is built around the systems you already run. Integration is defined during the assessment. Statutory recipes, tickets and emissions reporting remain yours.

Yes. One fiberglass line, one mineral-wool cupola, or one curing oven is usually the practical start. Measure that, then decide whether to widen.

Contact

Talk to an insulation expert

  • 30 minA focused conversation about the insulation problem you are trying to solve. No sales deck.
  • OutcomeA practical view of whether INSUS can help, what data would be needed and where it makes sense to start.
  • We will first understand your current process, what information you have and where the biggest gap is.
  • If the right answer is a cullet magnet, a density gauge, an oven zone or an existing system, that is what we will tell you.

Request a call

We reply within one working day, from a person, with a proposed time.